Ultra-Thin Wall Cap Molding: Achieving Sub-0.6mm Wall Thickness with Precision Tooling and Conformal Cooling
Ultra-Thin Wall Cap Molding: Achieving Sub-0.6mm Wall Thickness with Precision Tooling and Conformal Cooling
Published by cap-molds — Technical Whitepaper & Engineering Guide
Introduction: The Lightweighting Imperative in Closure Manufacturing
In the global rigid packaging sector, resin consumption accounts for up to 70% of total closure manufacturing costs. As FMCG brands and beverage packaging converters strive to reduce raw material usage, lower logistics carbon footprints, and hit aggressive ESG targets, lightweighting has moved from a competitive advantage to an industry standard. However, pushing bottle cap wall thickness below 0.6mm—entering the ultra-thin wall domain—presents severe molding and mechanical challenges.
Reducing wall stock dramatically narrows the injection processing window. Standard tooling architectures often suffer from core deflection, non-uniform melt fronts, premature freeze-off, and high differential shrinkage leading to cap warpage or seal failure. As a specialized China bottle cap mold manufacturer, cap-molds solves these critical production bottlenecks through sub-micron machining tolerances, specialized mold venting, high-injection-pressure mold steel structures, and advanced conformal cooling channels.
1. Structural Mold Integrity and Core Deflection Prevention
Injecting high-flow PP or HDPE resins into ultra-thin cavity spaces requires extreme injection speeds and pressures exceeding 2,000 bar. Under these conditions, asymmetrical melt flow creates high side-loads on core pins, leading to core shift, non-uniform wall thickness distribution, and dimensional instability.
Key Engineering Solutions for Core Stability:
- Dual-Guided Core Pin Alignment: Utilizing ultra-precise tapered interlocks and dual-guided neck ring assemblies maintains absolute concentricity between the core and cavity inserts under maximum injection tonnage.
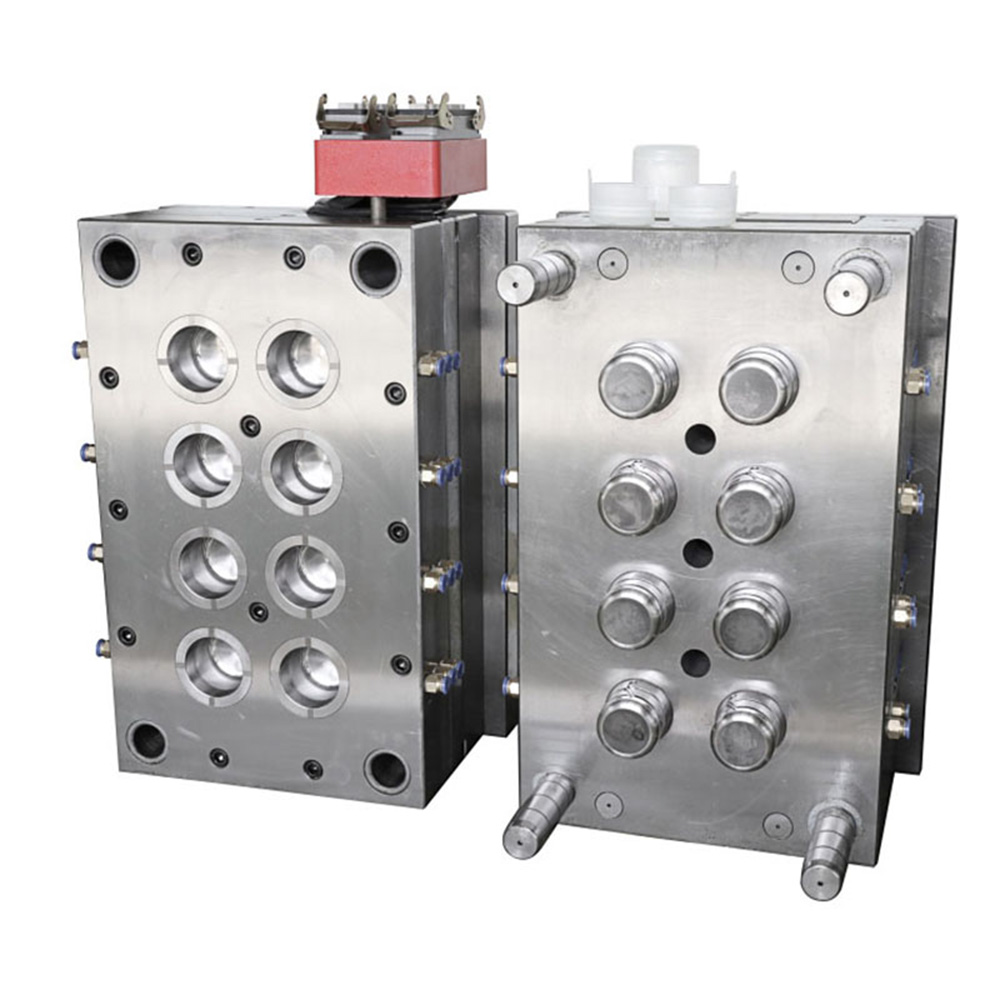
- High-Rigidity Mold Base Steel: Mold bases constructed from pre-hardened 4140 or S50C steel prevent structural deflection across high-cavitation layouts (32, 48, or 64 cavities).
- Sub-Micron Machining Tolerances: All core, cavity, and thread components are machined to tolerances within ±0.003mm, ensuring full interchangeability and identical flow resistance across all cavities.
2. Conformal Cooling and Rapid Thermal Dissipation
Because thin-walled caps contain significantly less thermal mass, heat must be extracted rapidly and uniformly to prevent stress-induced warpage and maintain cycle times under 4.5 seconds. Traditional straight-drilled cooling channels leave critical hotspots around deep core tips and thread profiles.
| Cooling Technology | Thermal Profile & Heat Transfer | Cycle Time Impact | Structural Quality Outcome |
|---|---|---|---|
| Standard Drilled Baffles | Uneven heat extraction; thermal hotspots at core tip | Baseline (5.5 – 6.5s) | Risk of ovality, thread distortion, and seal rim sink marks |
| Beryllium Copper (BeCu) Inserts | High conductivity pulls heat quickly away from thick zones | 15% – 20% Reduction | Improved seal lip stability and reduced internal stress |
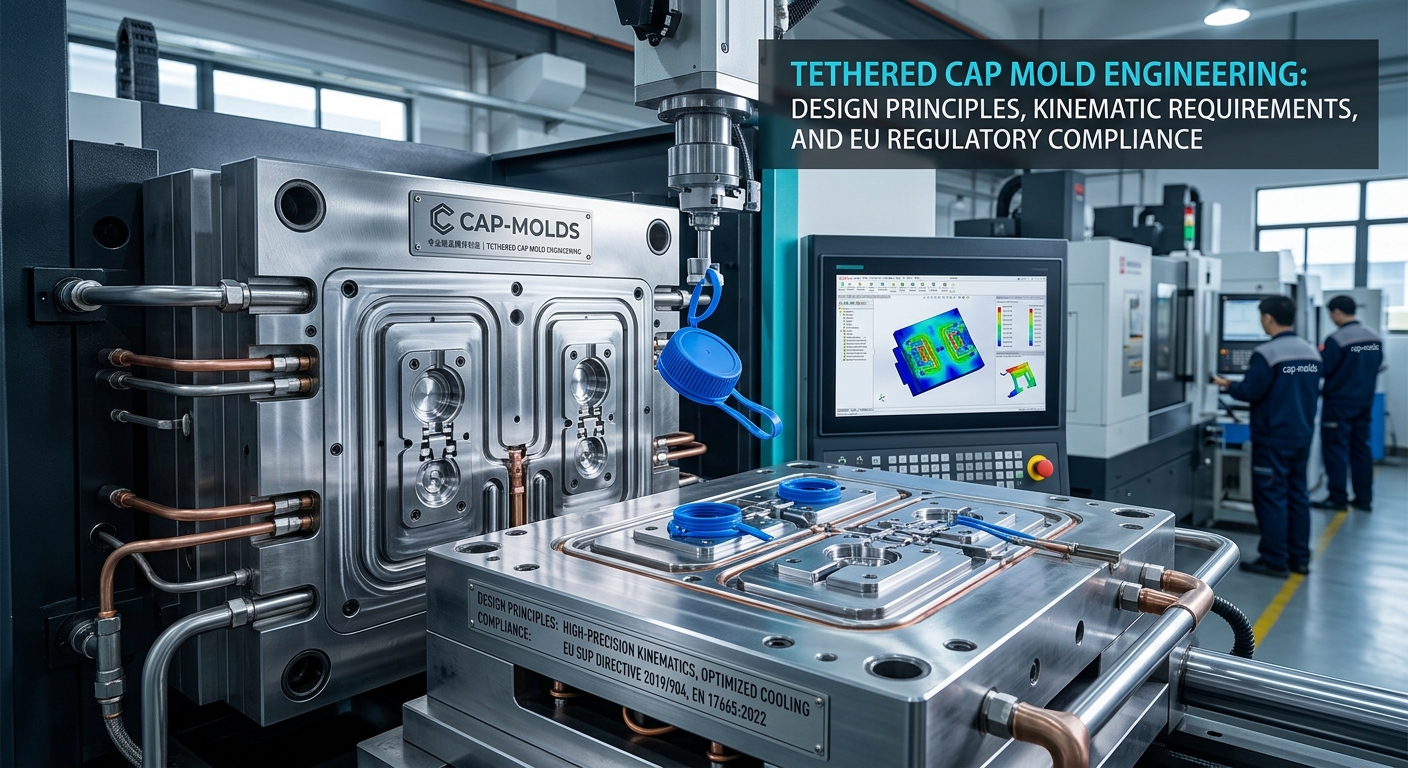
| cap-molds 3D Conformal Cooling | 3D SLM metal-printed channels contouring thread geometry within 1.5mm | Up to 30% Reduction (<4.5s) | Zero out-of-roundness; uniform shrinkage across sub-0.6mm walls |
3. Injection Dynamics, Melt Flow, and Micro-Venting Optimization
Thin-wall cap molding requires ultra-high flow velocity to fill the cavity before the polymer freeze-off layer develops. However, high-speed displacement of air inside the closed mold cavity can lead to severe diesel effect burn marks and short shots if air evacuation is restricted.
- Balanced Hot Runner Geometry: Manifold systems designed via Moldflow rheological simulation feature smooth internal radius bends and polished melt channels to minimize shear rate spikes and polymer degradation.
- Valve-Gated Precision Ingress: Hydraulic or pneumatic valve-gate systems ensure instantaneous opening and clean shut-off without pin drool or gate vestige, maintaining pristine top-seal surfaces.
- Micro-Venting Engineering: Strategic circumferential micro-vents (0.012mm to 0.018mm depth) along the parting line and core pins allow rapid gas discharge while completely preventing plastic flash.
4. Metallurgical Excellence and Wear-Resistant Coatings
Ultra-thin wall molds endure continuous cyclic shock under elevated injection pressures. To guarantee long mold lifespans exceeding 5 million shots, cap-molds enforces strict metallurgical criteria:
- Corrosion and Impact Resistant Steels: Core and cavity inserts are crafted from Swedish and German ESR-grade stainless steels (S136, Stavax, 1.2083) hardened to HRC 52–54.
- PVD & DLC Surface Coatings: Titanium Nitride (TiN) or Diamond-Like Carbon (DLC) coatings applied to moving slides, ejector pins, and core surfaces reduce friction coefficients below 0.1, eliminating wear particles and allowing dry-lube operation in cleanroom setups.
5. Quality Validation and Factory Acceptance Testing (FAT)
Before shipment, every ultra-thin wall cap mold undergoes rigorous multi-hour testing under full production conditions at the cap-molds facility.
FAT Protocol & Inspection Criteria:
- Continuous Ultra-Speed Runs: Testing at maximum injection speed and clamping force to verify cycle time stability (<4.5 seconds) and automatic drop functionality.
- Full CMM & Optical Scans: Laser measuring wall thickness uniformity across 100% of cavities to confirm variance remains under ±0.01mm.
- Seal Integrity & Drop Testing: Caps molded during trial runs undergo pressurized leak testing, torque testing, and drop resistance tests on commercial PET bottle neck finishes.
Partnering with cap-molds: The Global Thin-Wall Closure Specialist
At cap-molds, we specialize in high-speed, multi-cavity plastic bottle cap molds engineered for ultra-lightweight closures. Our complete solutions—from initial cap DFM and flow optimization to ultra-precision tooling and conformal cooling integration—help beverage brands and packaging converters achieve maximum material savings without sacrificing cap structural performance.